Gravity die casting · component page
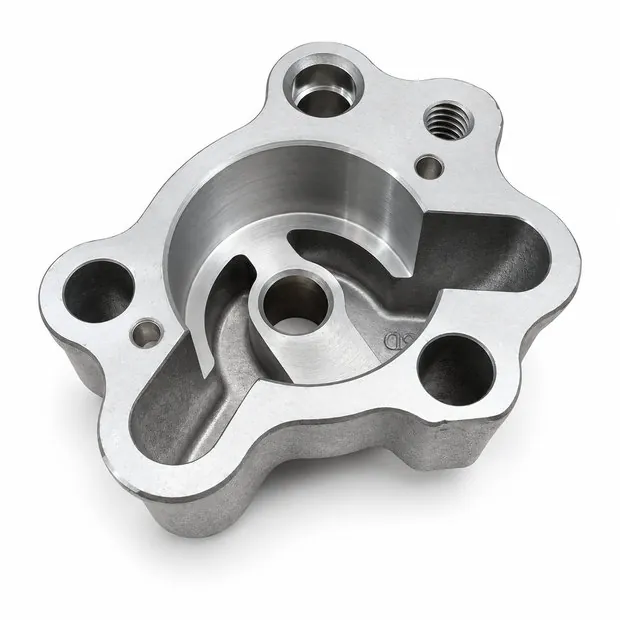
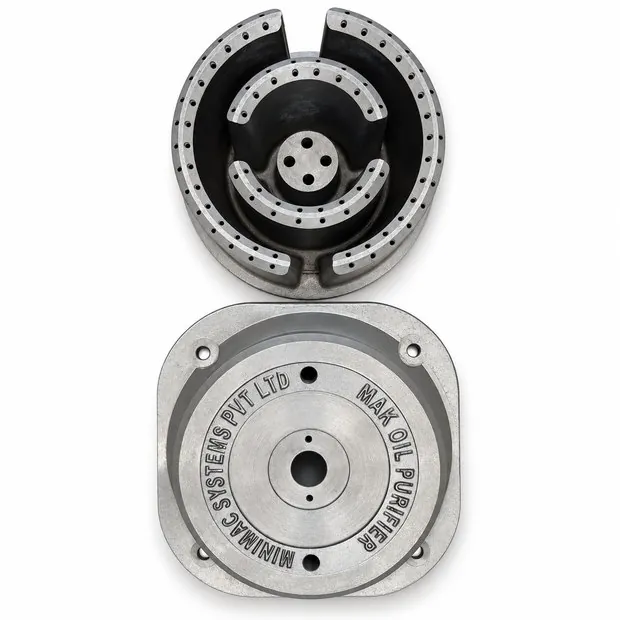
Machined pump housing
A fully machined pump housing is where casting and machining meet. The casting must give clean metal where the tools cut, with no porosity opening up in a bore or a sealing face, and enough machining stock to clean up without waste.
We cast and machine pump housings and filter bowls in house, so porosity found at machining is fed straight back to the casting process. Critical bores are air gauged on every part.
Process, alloys and indicative ranges
| Process | Gravity die casting; HPDC for thinner, smaller housings |
|---|---|
| Machining stock | Typically 0.8 to 1.5 mm per face, indicative |
| Alloys | LM25, LM6, LM13 |
| Supplied | Fully machined, ready to assemble |
Ranges are indicative for this kind of part. We confirm process, machine, alloy and tolerances for your design at drawing review.
Critical features and how we check them
| Bore diameters | Air gauging in house, on every part |
|---|---|
| Bore to face squareness and positions | Fixture checks in house; CMM through a partner on first articles |
| Porosity in machined faces | Visual inspection in house, at every stage; x ray in house during new component development |
| Pressure tightness | Leak test arranged through a specialist partner |
Machining and finishing options
- Turning and milling on CNC and VMC machines
- Ultrasonic cleaning on our seven tank line
- Sub assembly of plugs, inserts or seals to your bill of materials
Questions that sharpen your quote
- Which bores and faces are critical, and to what tolerance?
- Cleanliness requirement after machining?
- Leak test pressure and allowed leak rate?
Related
Similar parts
Family, process and industry
Have a machined pump housing to quote?Send the drawing and annual volume. An engineer replies within 48 hours.
Quote a part like this →