Gravity die casting · component page
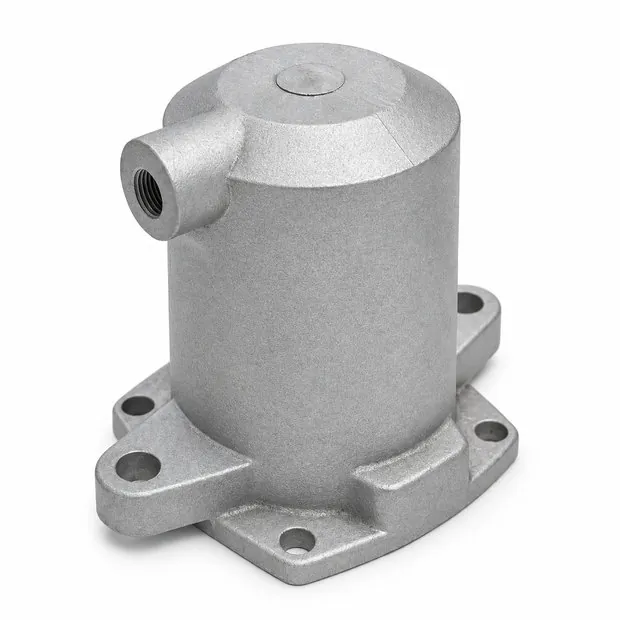
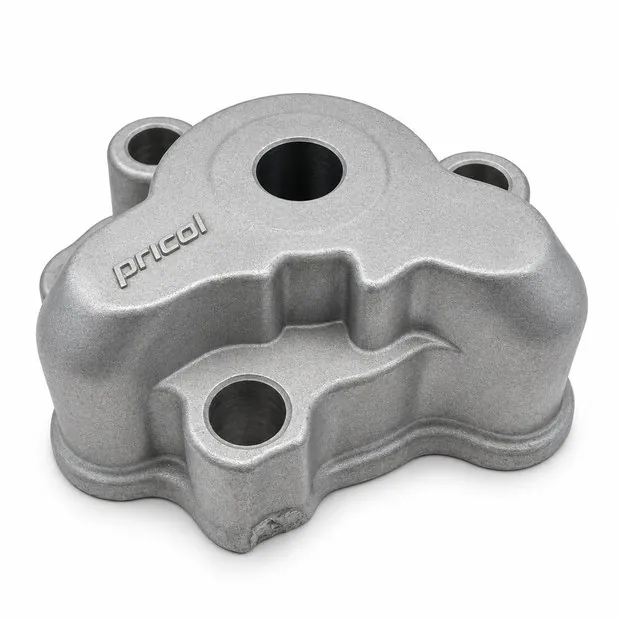
Flanged pump body
A pump body has to hold pressure, keep its sealing faces flat and keep the shaft bore in line with the volute. Thicker sections and internal passages make gravity die casting the usual choice, because the slower, quieter fill gives sounder metal than high pressure casting in these sections.
We gravity cast flanged pump bodies and pump covers, then machine flanges, sealing faces and bores in house. Where the drawing calls for pressure testing, leak testing is arranged through a specialist partner.
Process, alloys and indicative ranges
| Process | Gravity die casting, tilting or horizontal |
|---|---|
| Typical wall | 4 to 12 mm, indicative |
| Alloys | LM25, LM6, LM13 |
| Supplied | As cast, semi machined or fully machined |
Ranges are indicative for this kind of part. We confirm process, machine, alloy and tolerances for your design at drawing review.
Critical features and how we check them
| Shaft or seal bore | Air gauging in house, on every part |
|---|---|
| Flange face flatness and bolt pattern | Surface plate and functional gauge in house |
| Pressure tightness | Leak test arranged through a specialist partner |
| Internal soundness | X ray in house during new component development |
Machining and finishing options
- Flange, face and bore machining in house
- Heat treatment requirements agreed at enquiry, when the drawing calls for them
- Coating or painting through a partner
Questions that sharpen your quote
- Test pressure and medium for leak testing?
- Is impregnation allowed by your specification? We do not offer it in house today; a vacuum impregnation plant is planned.
- Heat treatment condition, for example LM25 TF?
Related
Similar parts
Family, process and industry
Have a flanged pump body to quote?Send the drawing and annual volume. An engineer replies within 48 hours.
Quote a part like this →