High pressure die casting · component page
Cast aluminium fan impellers
Impellers and vaned rotors turn at speed, so the hub bore, the vane geometry and the mass distribution matter as much as the casting itself. An impeller that is out of balance will vibrate, however good it looks.
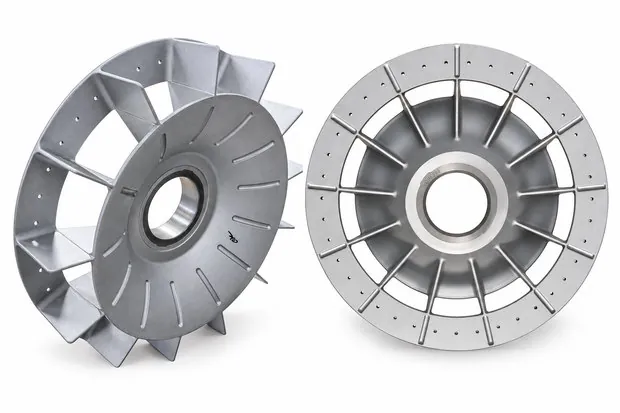
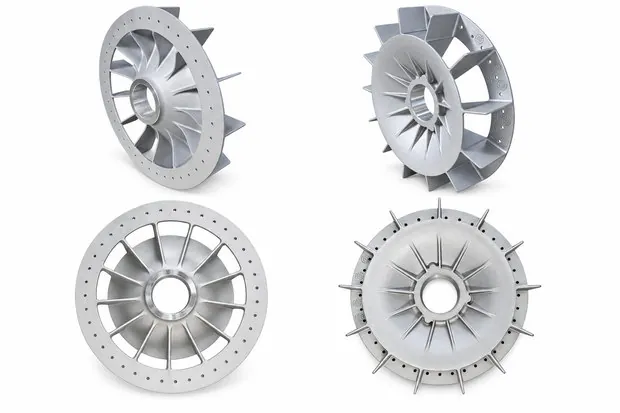
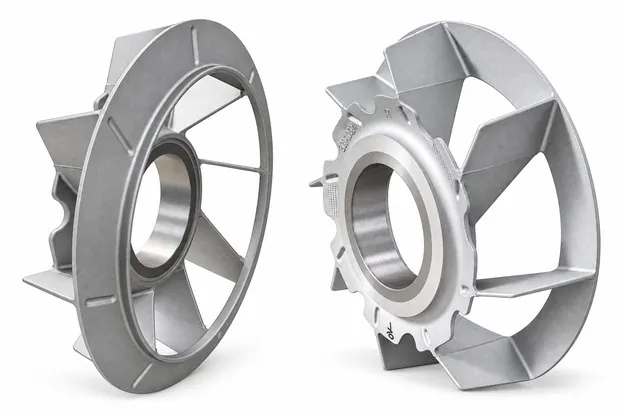
We high pressure die cast vaned fan impellers and rotors and machine the hub bore and keyway in house. The fettling bench in our process route shows impeller vanes being finished by hand, so each vane is clean and consistent before machining.
Process, alloys and indicative ranges
| Process | HPDC |
|---|---|
| Typical vane thickness | 1.5 to 3 mm, indicative |
| Alloys | ADC12, LM24, LM6 |
| Supplied | Cast and fettled, or bore machined |
Ranges are indicative for this kind of part. We confirm process, machine, alloy and tolerances for your design at drawing review.
Critical features and how we check them
| Hub bore diameter | Air gauging in house, on every part |
|---|---|
| Bore to outer diameter runout | Checked in house on a fixture; CMM through a partner on first articles |
| Vane completeness and flash | Visual inspection in house, at every stage |
| Hub soundness | X ray in house during new component development |
Machining and finishing options
- Hand fettling of vanes
- Bore and keyway machining
- Balancing to your grade can be discussed at enquiry; tell us the requirement
Questions that sharpen your quote
- Which balance grade, if any, does the drawing call for?
- Operating speed and temperature?
- Is the bore a press fit, a key or a taper lock?
Related
Family, process and industry
Have a cast aluminium fan impellers to quote?Send the drawing and annual volume. An engineer replies within 48 hours.
Quote a part like this →