Gravity die casting · component page
Engine timing cover
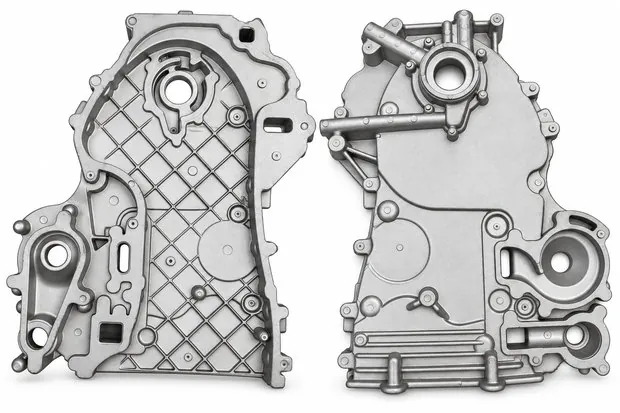
A timing cover closes the front of an engine and carries a seal bore for the crankshaft. Its sealing face must be flat over a long, thin flange, and the seal bore must sit in the right place relative to the dowels.
The timing cover in our gallery is gravity cast. For covers of this kind we machine the sealing face, seal bore and dowel holes, and check the bore on every part.
Process, alloys and indicative ranges
| Process | Gravity die casting; HPDC for thinner, high volume covers |
|---|---|
| Typical wall | 3.5 to 6 mm, indicative |
| Alloys | LM25, LM6, LM24 for HPDC |
| Supplied | As cast or machined |
Ranges are indicative for this kind of part. We confirm process, machine, alloy and tolerances for your design at drawing review.
Critical features and how we check them
| Seal bore | Air gauging in house, on every part |
|---|---|
| Sealing face flatness | Surface plate check in house |
| Dowel hole positions | Functional gauge in house; first article inspection on every new tool |
| Porosity at the sealing face | Visual inspection in house, at every stage |
Machining and finishing options
- Face, bore and hole machining
- Shot blasting
- Packing that protects the sealing face
Questions that sharpen your quote
- Gasket or liquid sealant on the face?
- Is the cover cast only or machined by us?
- Annual volume?
Related
Similar parts
Family, process and industry
Have a engine timing cover to quote?Send the drawing and annual volume. An engineer replies within 48 hours.
Quote a part like this →